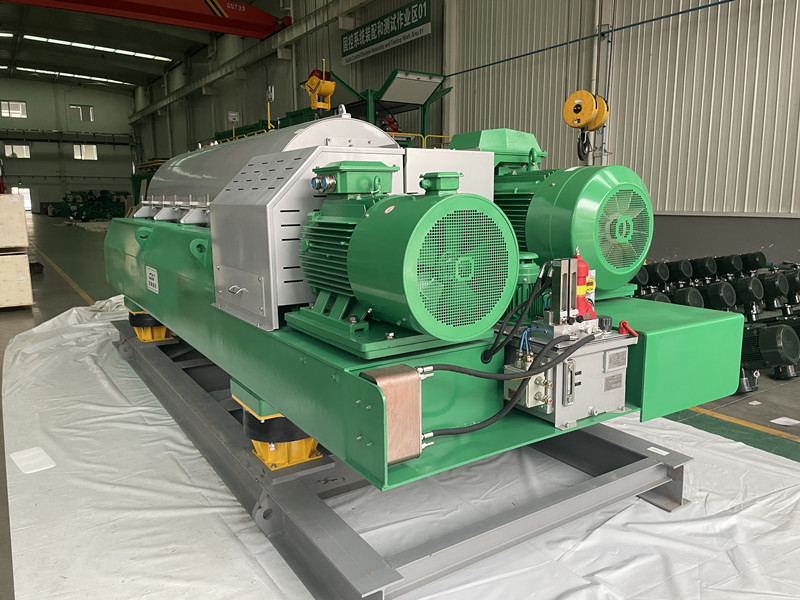
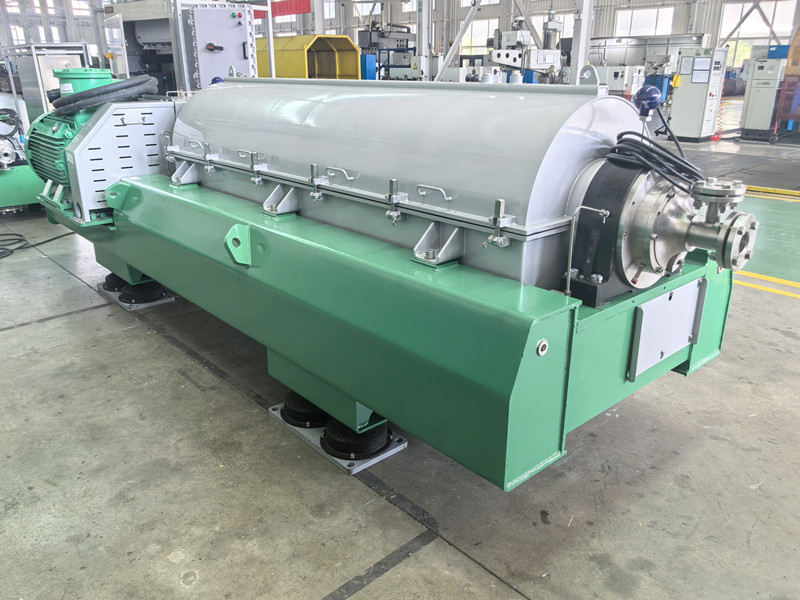
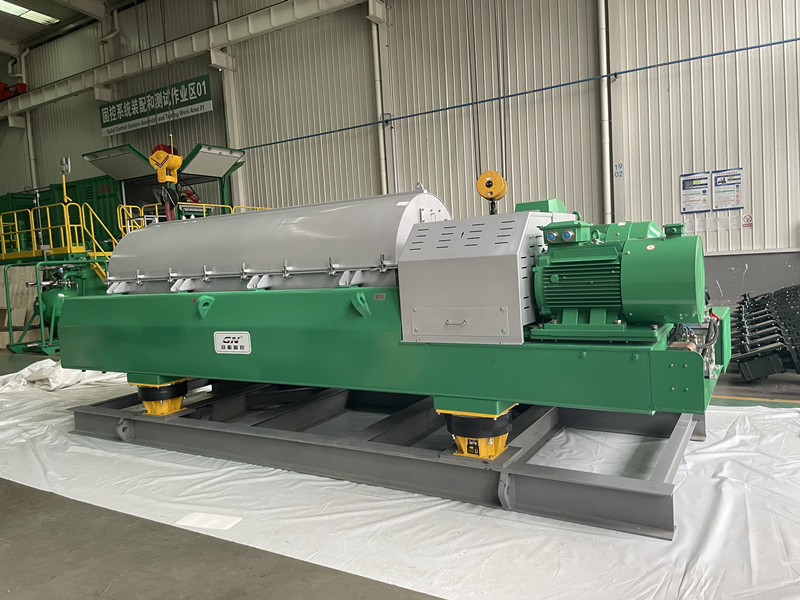
GN 30-inch Bowl Diameter Decanter Centrifuge for Domestic Mining Slurry Concentration Application

GN Separation officially launches its newly upgraded 30-inch large-bowl decanter centrifuge, specially customized for high-concentration mineral slurry thickening and dewatering in domestic mining projects. Breaking the limitation of small and medium-size centrifuges with low single-unit throughput, this large-diameter separation equipment delivers high-efficiency solid-liquid separation for metal ore, non-metal ore tailings slurry, coal washing slurry and mineral concentrate dehydration, providing an energy-saving, high-yield and fully automatic solution for domestic mining enterprises to realize tailings dry stacking and resource recycling.

Severe Pain Points of Traditional Mining Slurry Treatment in Domestic Mines

In recent years, domestic mining industry has raised stricter standards for tailings environmental treatment, resource recovery and production efficiency. Most medium and large mines adopt traditional thickener pools matched with small-size decanter centrifuges to treat mineral slurry, which bring multiple production bottlenecks:
  1. Low single machine processing capacity: Small-bowl centrifuges cannot cope with the massive slurry output of large-scale mines, requiring multiple units to work in parallel, leading to high equipment investment and complicated pipeline layout;
  2. Poor adaptability to high-concentration slurry: Fine mineral particles with high specific gravity are hard to be fully intercepted by conventional equipment, resulting in high water content of discharged solid tailings and low recovery rate of mineral concentrate;
  3. High operation and maintenance cost: Mining slurry contains a large number of hard rock particles with strong abrasion, ordinary centrifugal vulnerable parts wear rapidly and need frequent replacement, which affects continuous mining production;
  4. Large energy consumption and low automation level: Old-fashioned fixed-speed centrifuges cannot adjust operating parameters according to real-time slurry concentration, resulting in unnecessary power waste and relying on manual on-site operation for a long time.
In addition, the land occupation of tailings ponds is increasingly restricted by national environmental policies, so mining enterprises are in urgent need of large-capacity, high-dehydration-efficiency separation equipment to realize dry discharge of tailings and reduce the storage pressure of tailings ponds.

Core Technical Advantages of GN 30-inch Large Bowl Decanter Centrifuge

The 30-inch bowl diameter is the core design highlight of this model. Compared with conventional 22-inch, 26-inch centrifuges, the effective settling area inside the drum is greatly expanded, which prolongs the sedimentation time of mineral particles and significantly improves slurry treatment capacity and separation precision. Combined with targeted mining-oriented structural optimization, the equipment has prominent industry advantages:
  1. Ultra-large processing capacity to match large-scale mining production

    With a 30-inch integral forging rotary drum and optimized length-diameter ratio design, the maximum hourly processing capacity of mineral slurry reaches 80-120 cubic meters, which can replace 2-3 sets of medium-sized centrifuges. It simplifies the on-site layout of the slurry treatment system and reduces the overall investment of supporting facilities such as feeding pumps and pipelines for mine owners.

  2. High-strength wear-resistant structure adapted to abrasive mineral slurry

    The main drum is made of thickened duplex stainless steel, while the conveyor spiral surface is overlaid with tungsten carbide wear-resistant alloy. The slag outlet, feeding port and other flushing parts are equipped with replaceable high-chromium alloy bushings. Even under long-term continuous treatment of hard ore slurry such as iron ore, copper ore and coal gangue, the service cycle of vulnerable parts is increased by more than twice, cutting frequent shutdown maintenance losses for mines.

  3. Full-range VFD intelligent frequency conversion control system

    The complete set of variable frequency drive system realizes stepless independent adjustment of drum rotating speed and differential speed. Operators can adjust equipment operating parameters in real time according to slurry concentration, particle fineness and solid content of different ores. Whether it is concentrate thickening or tailings dehydration, the machine can maintain the optimal separation state, effectively reduce moisture content of solid slag and improve the recovery rate of useful minerals. The frequency conversion design cuts comprehensive energy consumption by 18%–25% compared with fixed-speed large centrifuges.

  4. Closed fully automatic operation, meeting domestic environmental protection standards

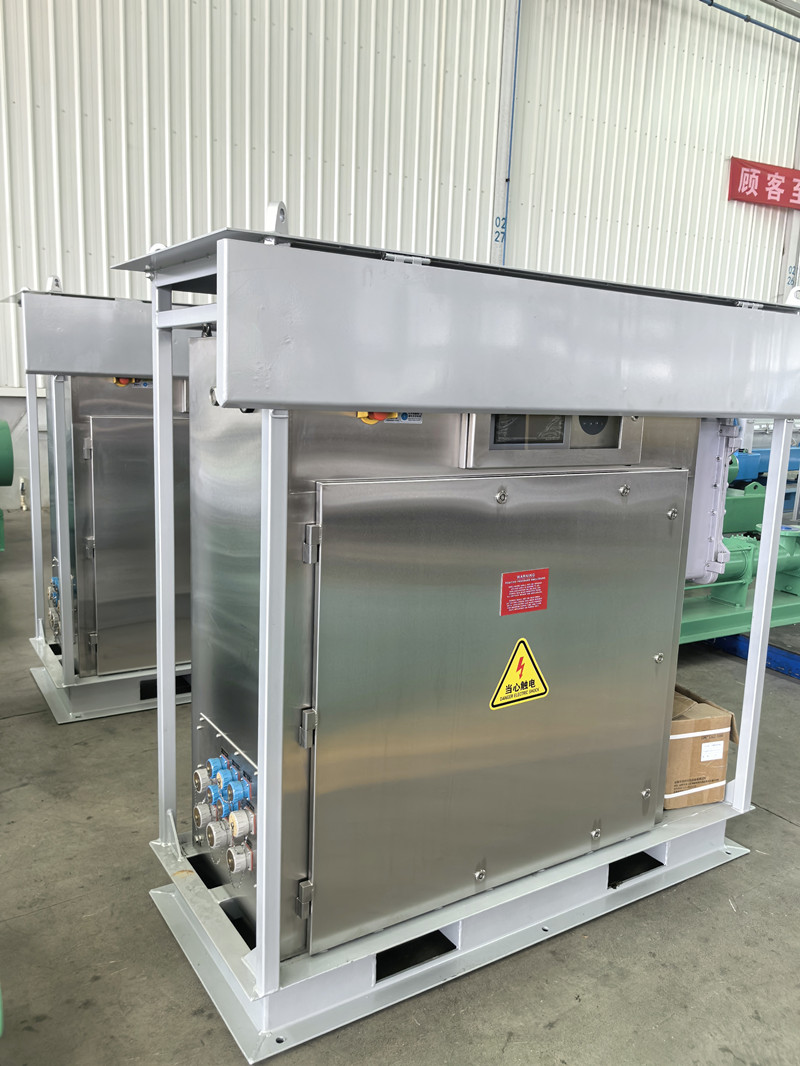
    The whole machine adopts fully sealed structural design to avoid slurry splashing and dust overflow during operation, without secondary pollution to the mine production area. Matched with GN self-developed PLC centralized control cabinet, it supports real-time remote monitoring of operating current, vibration, temperature and feeding flow, realizing unattended automatic operation and greatly reducing on-site labor configuration.
Practical Application Benefits for Domestic Mining Projects

After trial operation in multiple domestic iron ore and coal washing plants, the 30-inch large bowl decanter centrifuge achieves remarkable economic and environmental benefits:
  1. Mineral concentrate recovery rate increased by more than 12%, effectively improving mine resource utilization and economic output;
  2. Water content of discharged tailing slag stably controlled below 18%, dry slag can be directly transported for comprehensive utilization such as mine backfilling and building aggregate processing, greatly reducing the occupied area and safety risk of tailings ponds;
  3. Recycled clear water after separation can be fully returned to the ore washing production line, saving mine fresh water consumption and lowering water supply cost;
  4. Single machine covers large slurry treatment demand, simplifies the mine solid-liquid separation workshop layout and reduces the later equipment maintenance workload.

Market Prospect

The launch of GN 30-inch large bowl mining decanter centrifuge further enriches GN’s domestic mineral slurry separation product line. At present, GN’s full series of mining centrifugal separation equipment has been widely applied in coal washing, ferrous metal mining, non-ferrous metal mineral processing, rare earth ore and other domestic mining fields.
Facing the domestic mining industry’s general trend of green transformation, tailings dry discharge and intelligent production, GN Separation will continue to iterate large-size high-efficiency separation equipment, provide customized integrated slurry thickening and dehydration system solutions for domestic mining enterprises, and help the high-quality and low-carbon development of China’s mining industry.

Know more about GN Separation—GN 30-inch Bowl Diameter Decanter Centrifug
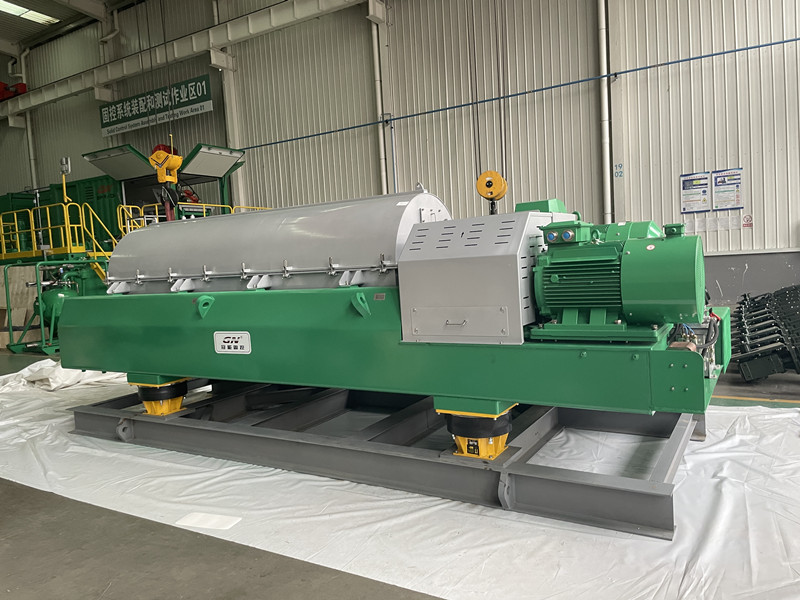
GN 30-inch Bowl Diameter Decanter Centrifuge for Domestic Mining Slurry Concentration Application

GN SOLIDS CONTROL recently supplied a 30-inch (760 mm) bowl diameter decanter centrifuge to a domestic mining operation for slurry concentration duty. This unit, model GNLW764A-VFD, represents a significant step in processing capacity for mine dewatering and especially tailings management.

The centrifuge features a bowl length of 3160 mm, yielding a length-to-diameter ratio of 4.2:1. This extended geometry provides prolonged residence time, which is essential for achieving fine solids capture in high-volume slurry streams. The unit handles up to 528 GPM (120 m³/h) at 20% solids content, making it suitable for large-scale mining operations where throughput directly affects production schedules.

Durability in abrasive mining slurries is addressed through tungsten carbide protection applied to the slurry distribution port, solids discharge port, and the screw conveyor surfaces. These wear-resistant measures extend service intervals and reduce maintenance downtime in continuous operation.

Beyond mining slurry concentration, GN’s bowl size serves tunnel boring mud cleaning, dredging slurry separation, industrial wastewater treatment, and municipal sewage sludge dewatering. The VFD-controlled unit allows operators to adjust bowl and differential speeds to match varying feed conditions, optimizing separation performance without mechanical modification.

This domestic installation demonstrates that large-diameter centrifuges, properly specified for the application, can provide reliable, high-capacity solids concentration in demanding mineral processing environments

GNLW554-VFD Decanter Centrifuge Delivers Proven Results for African Tank Bottom Oily Sludge Treatment

GN Separation is pleased to announce the successful deployment of its GNLW554-VFD large-bowl decanter centrifuge at a major tank bottom oily sludge treatment project in Africa. The installation marks another milestone in the company’s expanding footprint in the African oil & gas and industrial wastewater treatment sectors.

Addressing a Persistent Industry Challenge

Tank bottom oily sludge — a complex mixture of crude oil residues, water, and solid sediments that accumulates in storage tanks — has long presented operators with significant environmental and economic challenges. Traditional treatment methods are often labor-intensive, inefficient, and costly, particularly in remote African field locations where infrastructure and logistics constraints add further complexity.
High levels of free fatty acids (FFA) and varying solid compositions further complicate separation processes, requiring equipment that can adapt dynamically to changing feedstock characteristics.

The GNLW554-VFD Solution

Deployed as the core separation unit in the treatment train, the GNLW554-VFD decanter centrifuge has demonstrated exceptional performance across key operational metrics:
  • High-Capacity Bowl Design: The 550mm diameter large bowl delivers enhanced processing throughput while maintaining superior separation efficiency, enabling the client to handle substantial sludge volumes within tight project timelines.
  • Variable Frequency Drive (VFD) Technology: The fully adjustable VFD control system allows operators to fine-tune bowl speed and differential speed in real time, optimizing separation performance for varying sludge consistencies, FFA levels, and oil recovery targets.
  • Robust Construction: Built with wear-resistant materials and engineered for continuous-duty operation, the centrifuge excels in the harsh operating conditions typical of African oilfield environments.

Measurable Operational Benefits

Since commissioning, the system has delivered significant value to the client:
  • Maximized Oil Recovery: High-G-force centrifugal separation efficiently recovers reusable crude oil from the sludge stream, turning waste into revenue.
  • Reduced Waste Volume: Dramatically decreased sludge disposal volumes translate into lower hauling and landfill costs.
  • Environmental Compliance: Cleaner effluent discharge helps the operator meet stringent local environmental regulations.
  • Lower Operating Costs: Automated continuous operation reduces manual labor requirements and overall treatment costs per ton.

Expanding African Market Presence

This successful deployment reinforces GN Separation’s position as a trusted provider of solid-liquid separation solutions across Africa. The company’s equipment is already widely used in applications ranging from POME (Palm Oil Mill Effluent) treatment in West Africa to drilling mud processing and industrial wastewater projects continent-wide.
«Our GNLW554-VFD centrifuge was engineered specifically for challenging applications like tank bottom sludge treatment,» said a spokesperson for GN Separation. «The results from this African project validate our approach — robust equipment, intelligent controls, and real client value. We look forward to supporting more operators across the region in achieving their waste reduction and resource recovery goals.»
GN Separation is a leading manufacturer of decanter centrifuges, shale shakers, and complete solid-liquid separation systems serving the oil & gas, environmental, mining, and food processing industries worldwide.

HYDRAULIC DRIVE MUD CENTRIFUGE AND CUTTINGS DRYER FOR ASIA CLIENT

GN SOLIDS CONTROL recently has successfully shipped a full hydraulic drive decanter centrifuge and a vertical cuttings dryer to Asian customers. Both equipment address specific operational challenges in drilling fluid management and cuttings processing.

Unlike electrically driven units, GN’s hydraulic drive decanter centrifuge uses two independent hydraulic circuits to drive the bowl and the scroll conveyor separately. The hydraulic pump unit which driven by a single electric motor, feeds each circuit with its own pump and control system. Bowl speed and differential speed can be adjusted independently and continuously during operation, providing flexibility when processing variable mud weights or encountering changing downhole conditions.

The vertical cuttings dryer delivered alongside the centrifuge is designed specifically for drilled cuttings from oil-based and synthetic-based mud systems. Operating at 900 RPM, the unit generates 420 G of centrifugal force to separate liquid from solids. The stainless steel screen bowl retains the cuttings while allowing fluid to pass through the screen openings. Angled flights attached to the cone, rotating slightly slower than the bowl, extract the dried cuttings. Tungsten carbide hardfacing on the flights achieves HRC 65 hardness, significantly extending service life compared to conventional wear protection.

The delivery to Asian clients reflects growing recognition that properly specified solids control equipment—whether hydraulic drive centrifuges for demanding mud conditions or vertical dryers for efficient cuttings discharge—can improve fluid economics and reduce waste handling costs.

GN Potato Slices Flushing Water Starch Separation Centrifuge Gains Popularity Among Domestic Food Processing Plants

GN Special Centrifuge Realizes Efficient Starch Recovery from Potato Rinsing Wastewater, Empowering Domestic Potato Deep Processing Enterprises with Circular Economy Upgrade
July 3, 2026 – With increasingly stringent environmental protection requirements and rising raw material costs in China’s food processing sector, potato chip and french fry manufacturers are facing prominent problems of starch loss in slicing rinsing wastewater, high sewage treatment expenses and resource waste. Against this backdrop, the potato slices flushing water starch separation centrifuge independently developed and manufactured by GN Separation has been widely recognized and applied by numerous domestic food factories, delivering remarkable economic and environmental benefits for potato deep processing production lines.
In conventional potato processing workflows, large quantities of free starch dissolve into rinsing water after potato peeling, slicing and cleaning. Direct drainage not only increases organic pollutant load and wastewater treatment pressure for factories, but also results in massive wasted recoverable starch resources. Tailored to the physical properties of potato starch slurry, GN’s dedicated starch separation centrifuge adopts food-grade 304 stainless steel for all material contact components, fully complying with national food hygiene and production specifications. Equipped with complete CIP online automatic cleaning system, the unit effectively prevents material residue, bacterial reproduction and cross-contamination during long-term continuous food-grade production.
Based on high-speed centrifugal sedimentation principle, GN centrifuge continuously and automatically separates solid starch particles from potato slice flushing wastewater. Concentrated starch slurry separated out can go through subsequent dehydration, drying procedures for internal reuse in production or external sales as by-product to generate extra revenue. Meanwhile, clarified treated water can be recycled back to potato peeling, slicing and rinsing stations, cutting factory fresh water consumption by 30%~50%. Compared with traditional sedimentation tank and hydrocyclone separation processes, GN equipment features higher starch recovery rate (stable above 92% in field operation), smaller footprint, fully automatic unattended continuous operation, stronger adaptability to fluctuating wastewater flow and starch concentration, and more stable long-term separation performance.
Up to now, GN’s potato rinsing water starch separation centrifuges have been installed and put into stable operation in batches at many large, medium and small food processing plants located in major potato producing regions including Shandong, Henan and Inner Mongolia. End customers reported that the equipment helps them reduce sewage charges, lower water procurement costs and create incremental income from recovered starch, comprehensively lifting the overall profit level of potato deep processing projects.
Industry analysts commented that under the trend of energy conservation, emission reduction and resource recycling transformation in the food industry, GN customized separation equipment targeting potato processing wastewater starch recovery will become standard supporting configuration for newly-built and renovated potato chip and french fry production lines. Relying on independent technical advantages and mature on-site application experience, GN Separation will continue to launch targeted solid-liquid separation solutions for various food processing segments, facilitating the high-quality, low-carbon and circular development of domestic food manufacturing industry.